Powering Production: The Versatile Applications of a Modern Bottling Machine
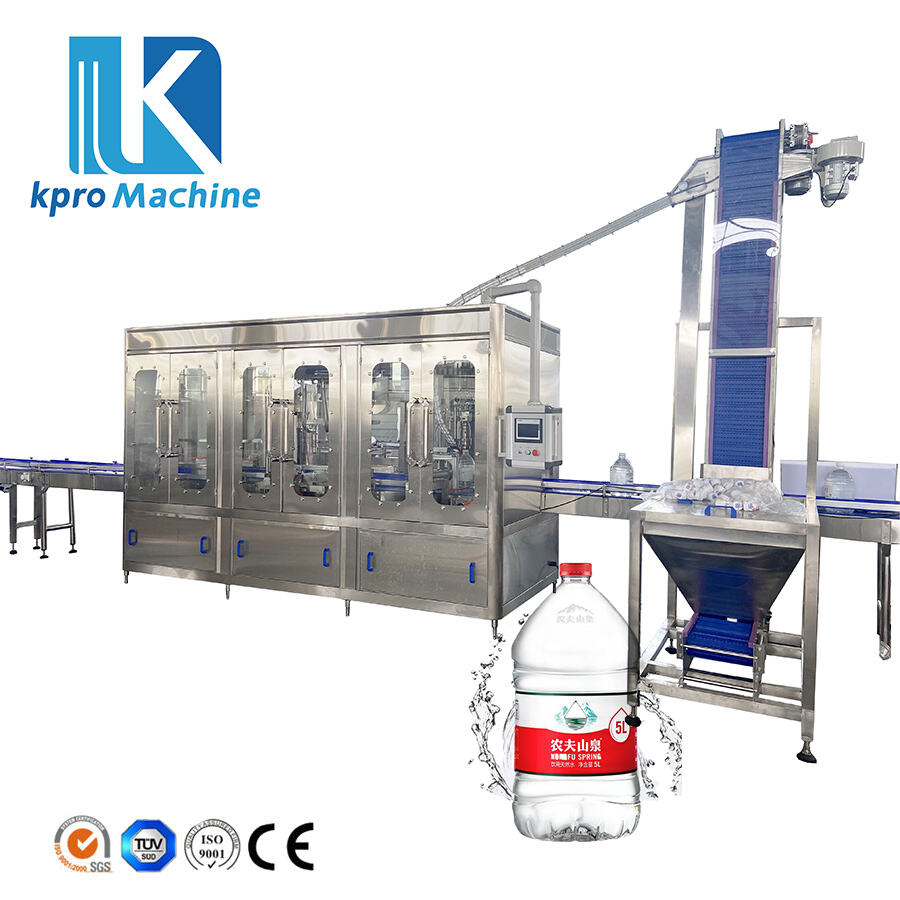
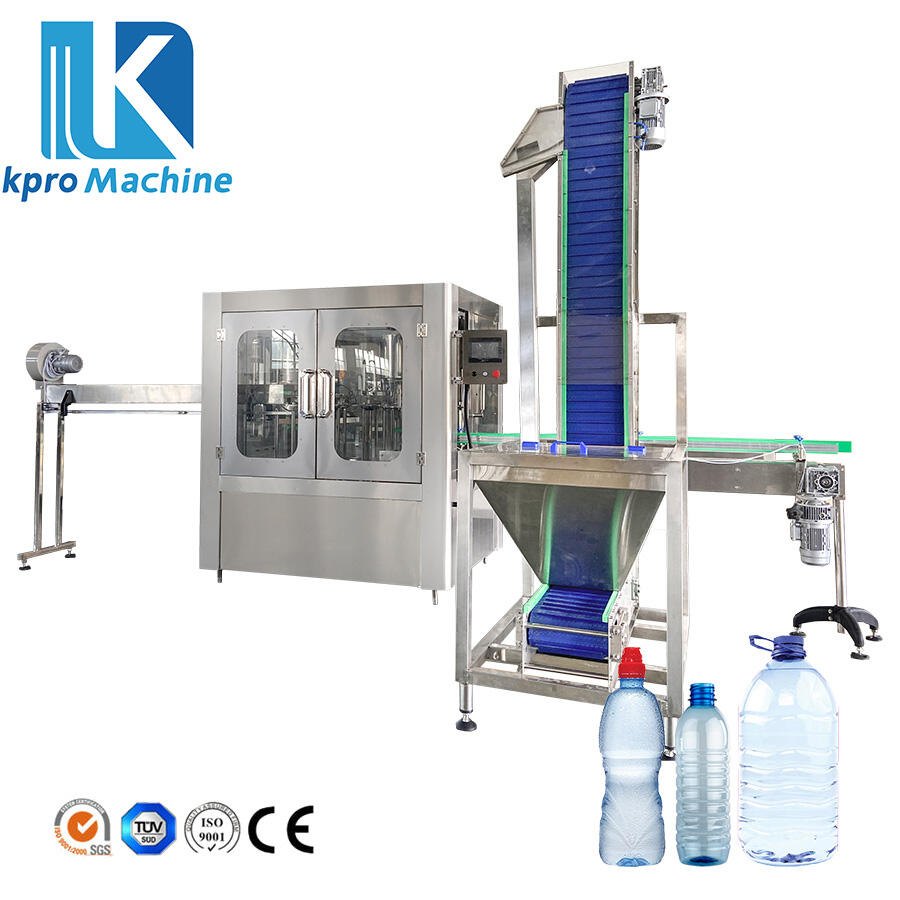
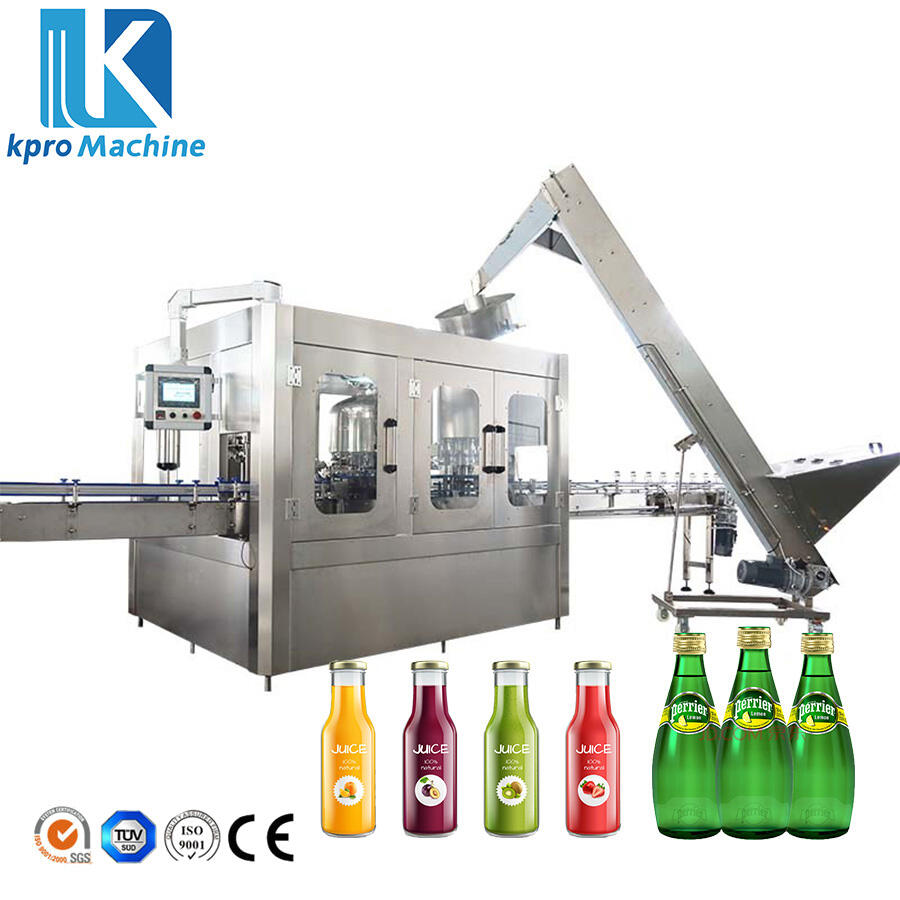
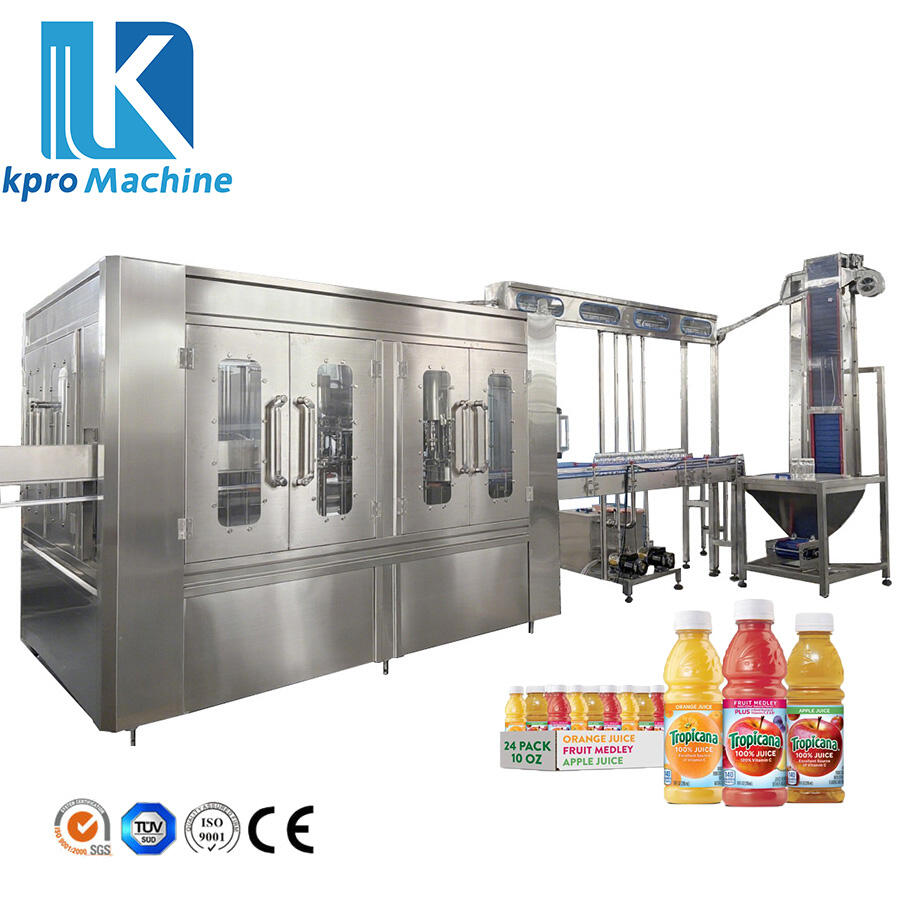
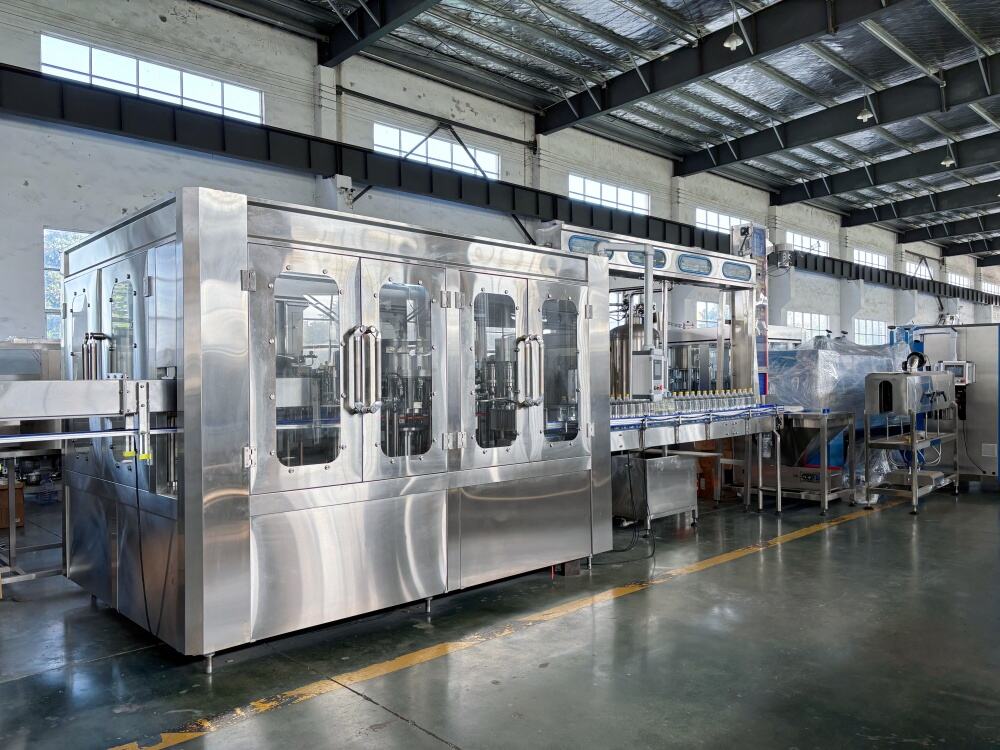
The most significant application of a bottling machine is within the global beverage industry. This is the core of high-volume, fast-paced production for a vast range of drinks, including water, carbonated soft drinks, juices, and ready-to-drink teas. Modern automated bottling lines handle everything from precise filling and capping to labeling with exceptional speed and accuracy. This ensures brand consistency, minimizes product loss, and meets the stringent hygiene standards required for consumable goods, making them indispensable for both major brands and emerging beverage companies.
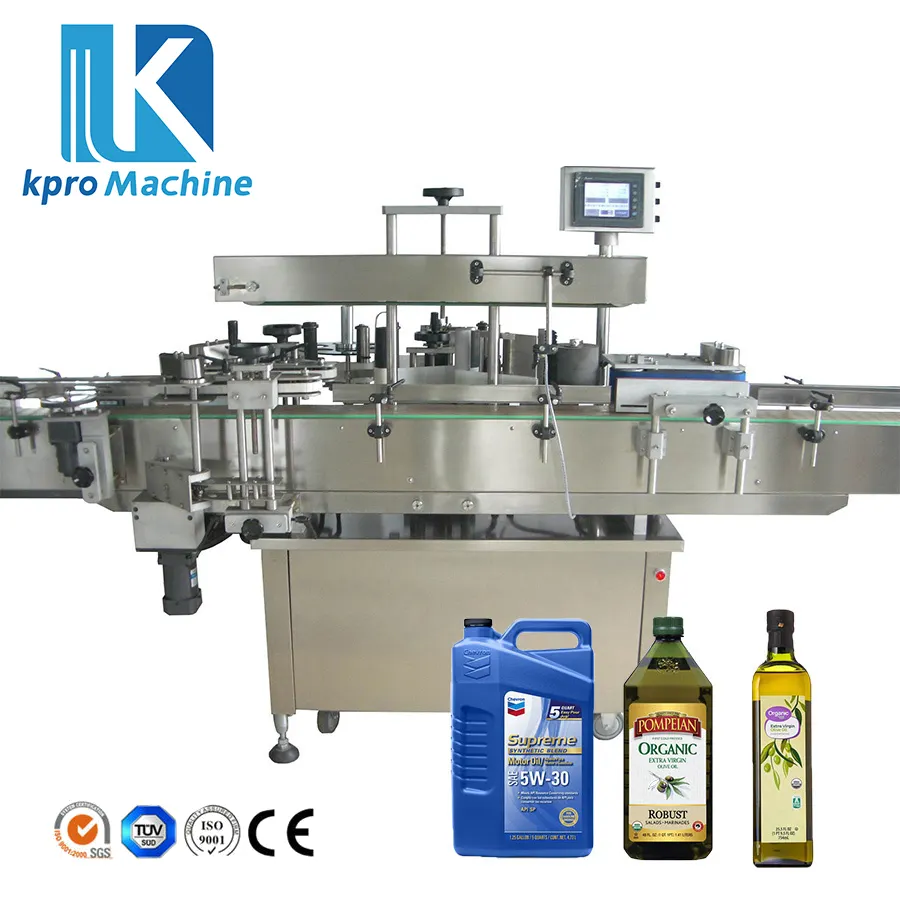
Beyond traditional beverages, bottling machines are crucial for the food, pharmaceutical, and chemical sectors. In food production, they are used for packaging cooking oils, sauces, syrups, and liquid dairy products. The pharmaceutical industry relies on sterile bottling machines for medications, syrups, and saline solutions, where precision and contamination control are non-negotiable. Similarly, the chemical industry uses chemically resistant machines to package products like motor oils, detergents, and solvents, demonstrating the technology's adaptability across diverse viscosity and safety requirements.
A growing application area is in supporting craft producers and sustainability initiatives. Small-scale and semi-automatic bottling machines enable craft breweries, distilleries, and artisanal food creators to scale their operations efficiently without a massive capital investment. Furthermore, as brands focus on reducing packaging waste, modern bottling equipment is adaptable for use with recycled materials and for filling reusable glass containers. This flexibility allows businesses of all sizes to meet evolving consumer demands for unique, local, and eco-conscious products.
 EN